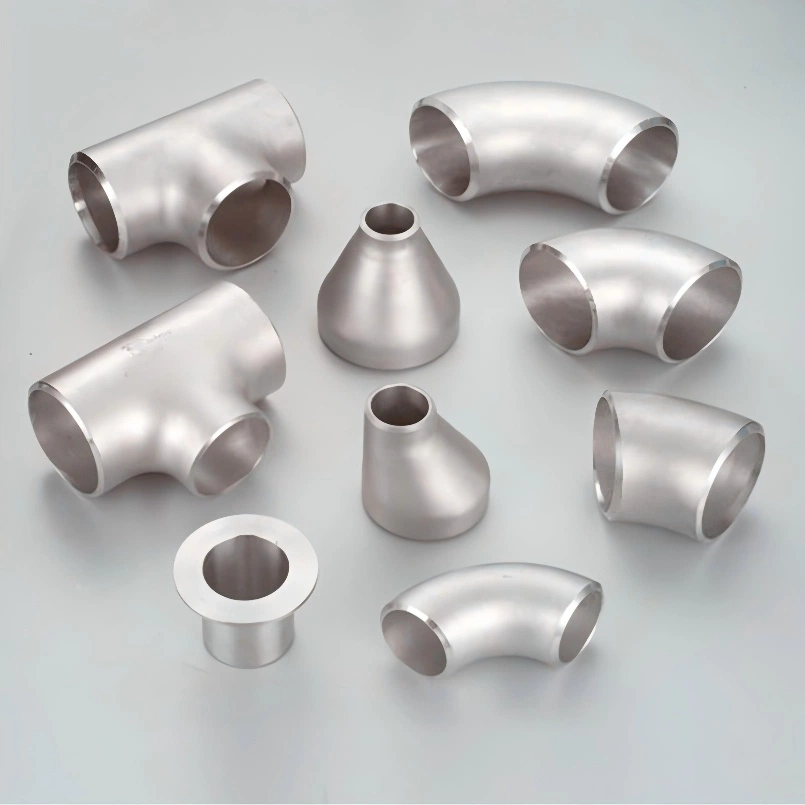
Butt weld pipe fittings join stainless piping with strong, leak-free welded joints — seamless SS304 / SS316L, full mill certificates. Designed for oil & gas, chemical, water treatment, shipbuilding, food and pharma piping projects where ANSI B16.9 dimensions and 3.1 mill certs are required.
Our butt weld pipe fittings are available in sizes 1/2″–48″ (DN15–DN1200). 90° / 45° elbows, equal and reducing tees, concentric and eccentric reducers, caps. Wall thickness SCH5S / SCH10S / SCH40S / SCH80S / SCH160S. Butt-weld bevel end per ANSI B16.25. For direction-change fittings see our dedicated butt weld elbow page; for the matching tube stock see seamless pipe and flanges. Tell us your size, schedule and quantity for a detailed quotation, size, schedule, material and quantity.
The main advantage of butt weld pipe fittings over threaded or socket-weld fittings is the ability to handle high pressure and high temperature applications. The smooth inner bore minimizes pressure drop and turbulence, making butt weld fittings ideal for process piping in chemical and petrochemical plants. Every fitting is fully dimensionally inspected with eddy-current test; PMI available. We directly serve EPC contractors and valve distributors across Southeast Asia (Indonesia, Malaysia, Thailand, Vietnam) and the Middle East (Saudi Arabia, UAE, Qatar, Kuwait).
🌏 Southeast Asia & Middle East Market Notes
Thailand / Vietnam food & beverage breweries: 316L fittings, DN25–DN100, SCH10S, Ra 0.8 µm polished — for CIP-cleaned process lines. Elbows, tees and reducers welded with ER316L filler, pickled after welding.
Indonesia / Malaysia palm oil & petrochemical: 316L seamless fittings, SCH40S, DN50–DN300 — for crude palm oil, cooling water and steam condensate. Reducers from DN200 to DN100 for pump suction lines.
Saudi Arabia / UAE seawater desalination & oil & gas: 316L butt-weld fittings, SCH40S, DN80–DN500 — for SWRO feed, brine discharge. Eccentric reducers on horizontal pump suction (flat side up) to avoid air pockets; concentric reducers on vertical lines.
Need a pre-fabricated piping spool — elbows + tees + reducers + flanges welded to your drawing, one heat number, one MTR?
Send Us Your Drawing →Fitting Type Comparison — When to Use Which
| Fitting | Function | Typical Use | Key Standard |
|---|---|---|---|
| 90° LR Elbow | Change direction 90°, long radius (1.5D) | Default direction change — pump discharge, process lines, low pressure drop | ANSI B16.9 |
| 90° SR Elbow | Change direction 90°, short radius (1.0D) | Tight skids, equipment connections where space is limited | ANSI B16.28 |
| 45° Elbow | Change direction 45° | Gradient lines, vent/drain runs, reducing sharp bends | ANSI B16.9 |
| Equal Tee | Branch line at 90° from main | Branch connections, sampling points, instrument taps | ANSI B16.9 |
| Reducing Tee | Branch smaller than main | Reducing branch for small-diameter instruments or drains | ANSI B16.9 |
| Concentric Reducer | Reduce size on vertical line, same centerline | Vertical piping, pump discharge to header size reduction | ANSI B16.9 |
| Eccentric Reducer | Reduce size on horizontal line, flat side top or bottom | Pump suction (flat top up, avoids air pockets), gravity drain lines (flat bottom down) | ANSI B16.9 |
| Cap | Close end of pipe | Blind end, future tie-off point, test closure | ANSI B16.9 |
Technical Specifications
| Size Range | 1/2″ – 48″ (DN15 – DN1200) |
| Types | 90°/45° LR & SR elbow, equal/reducing tee, concentric/eccentric reducer, cap |
| Wall Thickness | SCH5S / SCH10S / SCH40S / SCH80S / SCH160S |
| Material | 316L (1.4404) / 304L (1.4306) seamless; 304 / 316 / 321 on request |
| End Connection | Butt-weld bevel end (37.5° + 1.6 mm root face, per ANSI B16.25) |
| Standard | ANSI B16.9, B16.28, MSS SP-43, EN 10253-4 |
| Surface Finish | Pickled satin standard; polished Ra 0.8 µm for food pharma |
| Temperature Range | -29°C ~ +425°C (material dependent) |
| Testing | full dimensional, eddy-current and PMI XRF per EN 10204 |
| Material Certificates | EN 10204 3.1 MTC included per heat; PED 2014/68/EU, CE on request |
Dimension Table — 90° LR Elbow Center-to-End A (mm, ANSI B16.9)
| NPS | DN | OD (mm) | A (LR 1.5D) mm |
|---|---|---|---|
| 1/2″ | 15 | 21.3 | 38 |
| 3/4″ | 20 | 26.9 | 38 |
| 1″ | 25 | 33.7 | 38 |
| 1 1/4″ | 32 | 42.4 | 48 |
| 1 1/2″ | 40 | 48.3 | 57 |
| 2″ | 50 | 60.3 | 76 |
| 2 1/2″ | 65 | 73.0 | 95 |
| 3″ | 80 | 88.9 | 95 |
| 4″ | 100 | 114.3 | 102 |
| 5″ | 125 | 139.7 | 127 |
| 6″ | 150 | 168.3 | 152 |
| 8″ | 200 | 219.1 | 203 |
| 10″ | 250 | 273.0 | 254 |
| 12″ | 300 | 323.8 | 305 |
* For tee through-length, reducer O/H dimensions and cap wall thickness, contact us for complete drawings per ANSI B16.9.
🧮 Worked Example: Pre-fabricated Suction Spool for a Bangkok Dairy Plant
Project: Milk pump suction line, DN80 (3″), 316L seamless, SCH10S, Ra 0.8 µm polished. Layout: tank outlet → eccentric reducer DN100×80 flat-top → straight 500 mm → 90° LR elbow DN80 → pump flange. CIP temperature 85°C, milk product at 4°C.
Step 1 — Eccentric reducer orientation: On horizontal suction, the flat side of the eccentric reducer must face top. This prevents air pockets from forming at the top of the reducer — trapped air causes pump cavitation and milk product aeration. If flat side is down, the centerline slopes up and creates a high point.
Step 2 — Fitting count for the spool: 1 eccentric reducer DN100×80 (length H = 76 mm per B16.9), 1 LR 90° elbow DN80 (A = 95 mm). Total face-to-face between tank flange and pump flange = 76 + 500 straight + 95 = 671 mm. We pre-fabricate this spool in our workshop with one heat number, then ship as a single welded unit.
Step 3 — Wall thickness check (SCH10S vs SCH40S): For dairy at 4–85°C, max pressure 6 bar, SCH10S (t = 2.11 mm on DN80) is more than adequate by Barlow formula. SCH40S would add 50% cost and weight for zero benefit. Specify SCH10S for hygienic low-pressure duty.
Step 4 — Documentation: Each fitting ships with EN 10204 3.1 MTR certifying heat number, chemistry (C≤0.030%, Mo 2.0–2.5%), PMI result. After field welding, we supply the welder’s WPS/PQR and can arrange third-party RT or PT inspection if required by the HACCP audit. All wetted surfaces are pickled after welding and passivated to remove free iron.
⚠️ 4 Common Mistakes When Ordering Butt-Weld Fittings
Mistake 1 — Specifying SR elbow when LR would fit: SR (1.0D) creates 30% more pressure drop and turbulence. It should only be used where the layout physically cannot fit LR. Many suppliers push SR because it is cheaper to manufacture — but for process piping, LR is the default.
Mistake 2 — Using concentric reducer on horizontal pump suction: A concentric reducer on a horizontal line creates a high point at the top where air collects. This causes cavitation, noise and pump damage. Use eccentric reducer flat-top-up for all horizontal suction lines.
Mistake 3 — SCH mismatch between fitting and pipe: If the fitting is SCH40S and the pipe is SCH10S (or vice versa), the internal bore has a step at the weld root. This causes turbulence, erosion and stress corrosion. Always match schedule across pipe, fittings and flanges on the same spool.
Mistake 4 — Forgetting to request the 3.1 MTR: Without EN 10204 3.1, you cannot defend material grade in an audit, insurance claim or piping failure investigation. The MTR must list the heat number, chemistry, mechanical properties and test results. Without it, 304 vs 316L is visually indistinguishable.
📋 Commercial Terms
Payment: T/T 30% deposit + 70% before shipment; L/C at sight accepted for large orders. PayPal for sample orders.
Warranty: 12 months after shipment for material and manufacturing defects — covers dimensional non-conformance, wall thickness non-conformance, material chemistry mismatch and weld seam defects on seamless stock. Damage from field welding beyond WPS, abrasive media beyond specified limits, or coastal corrosion from failed passivation is not covered.
Packaging: Export plywood case; fumigation-free wooden pallet; bevel ends protected with plastic caps to prevent transit damage.
Shipping Documents: EN 10204 3.1 MTC per heat, PMI report, eddy-current test report, packing list, commercial invoice; certificate of origin on request.
Shipment Port: FOB Ningbo / Shanghai, China; CIF / DAP available on request.
Third-Party Inspection: SGS / Bureau Veritas / Intertek pre-shipment dimensional / PMI inspection supported at buyer cost.
Need Sizing Help or a Quote?
Send size (DN), pressure (PN/ANSI), material (304/316L), seat (EPDM/Viton) and quantity — we reply within 24 hours.
Get Free Quote »FAQ
Long radius (LR) or short radius (SR) elbow — which do I need?
LR (1.5D center-to-end) is the industry default — smoother flow, lower pressure drop, preferred for pump suction, viscous fluids and slurry. SR (1.0D) is used only where space is tight (tight skids, equipment connections). Unless your layout physically cannot fit LR, always specify LR.
Which wall thickness (SCH) do I choose?
For normal water / air / non-critical chemical at PN16, SCH10S is enough. For oil & gas, steam, high pressure or process corrosion, use SCH40S minimum. Sub-sea, high pressure or sour service requires SCH80S / SCH160S. Always match your pipe wall.
Seamless or welded (ERW) butt-weld fittings?
We supply seamless only. Seamless has no longitudinal weld, so there is zero risk of weld seam corrosion in chemical service and full pressure integrity. For pharma, food, offshore and sour service, seamless is mandatory.
How is the end bevel prepared for welding?
All fittings come with a standard bevel end per ANSI B16.25 — 37.5° bevel, with a 1.6 mm ±0.8 mm root face. Before welding, grind off the bevel area 20 mm either side to bright metal, then TIG root + fill.
304 / 304L vs 316 / 316L — which material?
304L is for general water, HVAC and mild chemicals. 316L adds molybdenum for chloride / coastal / bleach / marine service. For pharma / food / outdoor / coastal projects, always specify 316L.
Do you supply pre-fabricated welded spools?
Yes — we pre-fabricate complete spools in our workshop to your drawing, with one heat number, one MTR, NDT (RT/PT) on request. We ship the spool as a single welded unit, ready to bolt into place. This saves field welding time and ensures material consistency.
MOQ, stock and lead time?
MOQ is 1 piece. DN15–DN100 SCH10S / SCH40S in 304 are usually in stock (7 days). DN125+, 316L, special schedule or non-standard dimension takes 20–35 days. We can bundle fittings with flanges and seamless pipe into one shipment.
What is your warranty period?
We provide a 12-month warranty after shipment for material and manufacturing defects. This covers dimensional non-conformance, wall thickness non-conformance, material chemistry mismatch and weld seam defects on seamless stock. Damage from field welding beyond WPS, abrasive media beyond specified limits, or field modifications is not covered. Always provide the heat number from the EN 10204 3.1 MTC when raising a warranty claim.
📚 Further reading:
• Butterfly Valve Selection Guide (Size, Pressure, Material)
• How to Select a Wafer Butterfly Valve for Seawater Service
• Wafer Check Valve vs Swing Check Valve (2026 Guide)
You May Also Need
Related Technical Guides
Request a Quote for This Butt-Weld Elbow
Tell us the size, pressure and quantity you need. We reply within one working day.
Need a Custom Valve or Fitting?
Send us your specs: pressure, size, material and quantity — our engineers will reply within 24 hours with a detailed quotation. MOQ 1 piece.
FOB Ningbo / Shanghai · 5–10 days to Southeast Asia · 15–20 days to the Middle East · We reply within 24 hours (usually same business day)
Commercial terms: T/T 30% deposit + 70% before shipment, L/C at sight · export plywood case / fumigation-free pallet · 12 months warranty after shipment for material and manufacturing defects · EN 10204 3.1 MTC + API 598 test report + packing list + commercial invoice with every order · SGS / Bureau Veritas / Intertek pre-shipment inspection available
Get Free Quote »