Stainless Steel Pipe Fittings: Types, Standards & Applications
The complete 2026 guide to stainless steel pipe fittings — elbows, tees, reducers, caps, stub ends; butt-weld vs socket-weld vs threaded vs tri-clamp end connections; 304 vs 316L materials; ASME B16.9 vs EN 10253 vs JIS standards; Schedule wall thickness; concentric vs eccentric reducers; and a buying checklist for Southeast Asia and the Middle East EPC projects.
* Standard lead time depends on order quantity and destination country. 5–10 days to Southeast Asia, 15–20 days to the Middle East.
Quick Answer
For most general-industry stainless piping in Southeast Asia and the Middle East, specify ASME B16.9 butt-weld fittings in 304 / 304L Schedule 40S — elbows, equal tees, concentric reducers, caps, and stub ends. Switch to 316L Schedule 40S for coastal, brine, or corrosive service (Gulf seawater, palm-oil effluent, food/pharma wetted lines). On horizontal pump suction lines, ALWAYS use an eccentric reducer installed flat-side-up — a concentric reducer traps an air pocket and causes cavitation. Match the fitting Schedule and standard exactly to the pipe — welding mismatched ODs is the #1 cause of rework on new projects.
Key Takeaways
- Type: Elbows (90° / 45°) · equal / reducing tees · concentric / eccentric reducers · caps · stub ends.
- End connection: BW for DN50+ · SW for small high-pressure · threaded for utility · tri-clamp for hygienic.
- Material: 304L = general · 316L = coastal / brine / chemical / food-pharma · A234 WPB = oil/gas/steam.
- Reducer orientation: Eccentric flat-side-up on horizontal pump suction — concentric only on vertical / gas lines.
On This Page
1. Common Fitting Types
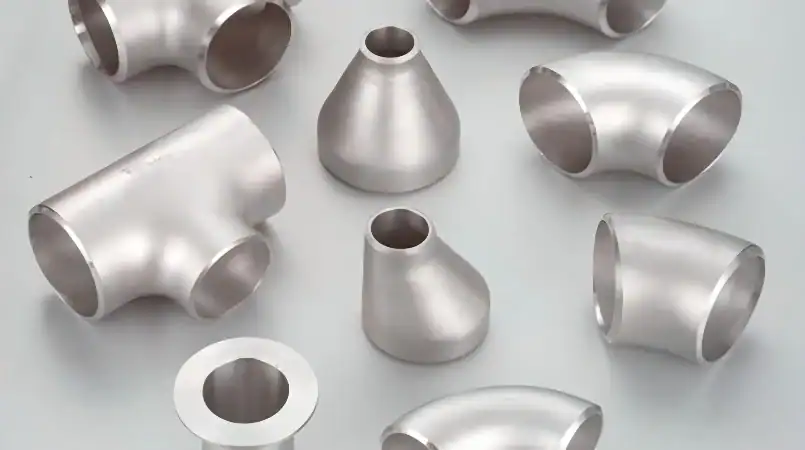
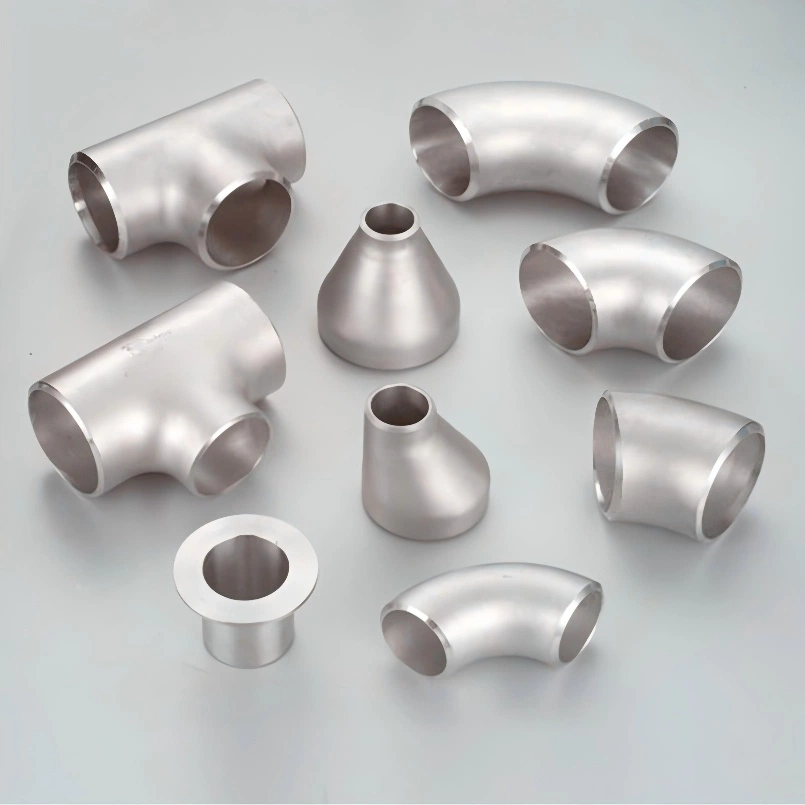
Stainless steel pipe fittings are the building blocks of any piping system. As a stainless steel pipe fittings manufacturer with experience since 2009, we’ll break down the most common types:
| Fitting Type | What It Does | Common Sizes |
|---|---|---|
| 90° Elbow | Changes direction by 90° | DN15 – DN600 (½” – 24″) |
| 45° Elbow | Changes direction by 45° | DN15 – DN600 |
| Tee (Equal) | Splits flow into two branches (same size) | DN15 – DN600 |
| Tee (Reducing) | Splits flow into two branches (different size) | DN15 – DN300 |
| Concentric Reducer | Reduces pipe size (centerline aligned) | DN15 – DN600 |
| Eccentric Reducer | Reduces pipe size (one side flat — no air pockets) | DN25 – DN600 |
| Coupling (Sleeve) | Connects two pipes of the same size | DN15 – DN300 |
| Cap | Closes the end of a pipe | DN15 – DN600 |
| Stub End | Used with lap-joint flanges (rotatable flange) | DN15 – DN600 |
See our full range of butt weld pipe fittings and butt weld elbows.
2. End Connection Types
| Connection Type | How It Connects | Best For |
|---|---|---|
| Butt-Weld (BW) | Welded directly to the pipe end | Permanent joints, high pressure / temp, no leak risk |
| Socket-Weld (SW) | Pipe slides into a socket, then fillet welded | Small sizes (DN50 and under), high pressure, easy alignment |
| Threaded (NPT / BSPT) | Screwed onto threaded pipe | Small sizes, low pressure, easy assembly / disassembly |
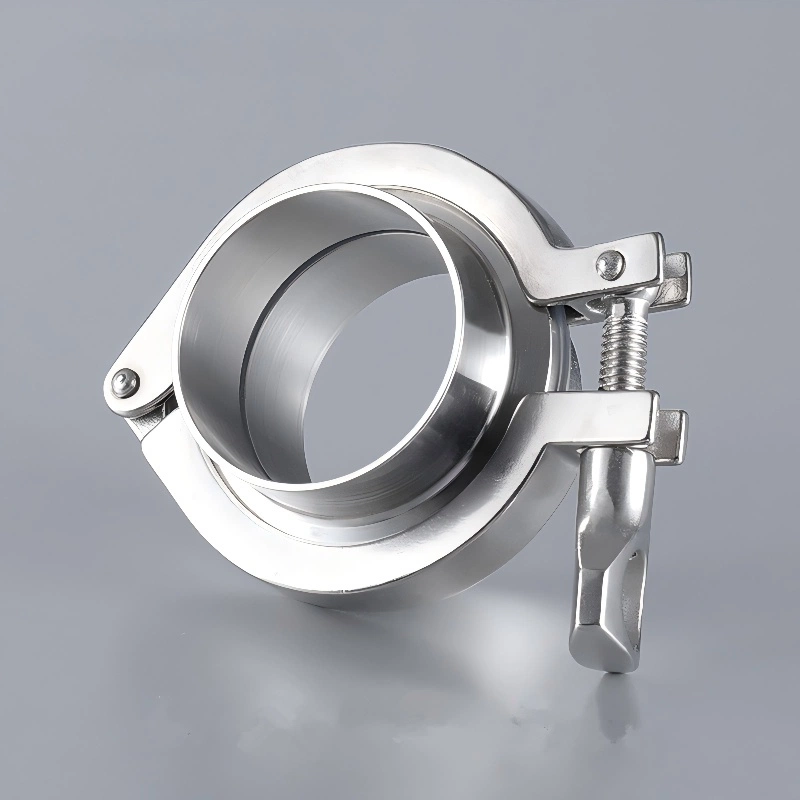
| Tri-Clamp (Sanitary) | Clamped together with sanitary clamp and gasket | Food, beverage, pharma, hygienic applications |
Most common for industrial: Butt-weld (BW) for DN50 and up, socket-weld (SW) for small high-pressure sizes. Threaded for low-pressure utility lines. Tri-clamp for hygienic applications — see our sanitary pipe fittings.
3. Material Options
| Material | Grade | Relative Cost | Best For |
|---|---|---|---|
| 304 / 304L | CF8 / CF3 | Medium | General industry, water, food, chemical (non-chloride) |
| 316 / 316L | CF8M / CF3M | Higher | Corrosive chemicals, coastal, saltwater, food / pharma |
| Carbon Steel (A234 WPB) | WCB | Lowest | Oil, gas, steam, general industry (non-corrosive) |
Rule of thumb: For general industrial use, 304 is fine. For coastal areas, saltwater, or corrosive chemicals, use 316L. For oil / gas / steam, use carbon steel (cheaper). Always specify whether you need 304 or 316 — they look the same but have a meaningful cost difference. Pair with stainless seamless pipes of matching material and Schedule.
4. Worked Example: Ho Chi Minh Water Plant Pump Suction Cavitation Fix
Step 1 — Problem
A 100,000 m³/day drinking water treatment plant in Thu Duc, Ho Chi Minh City had 4 × raw-water pumps (DN250 discharge, DN300 suction) taking water from the Saigon River. Six months after commissioning, operators reported: (1) loud rattling noise from pump #2 suction, (2) flow rate dropped 15% on pumps #1, #2, #3, (3) maintenance found pitting and erosion on the impeller eyes — classic cavitation damage. Pump #2 had to be shut down after 8 months.
Step 2 — Root cause analysis
The original piping spec used a concentric reducer DN300 → DN250 on the horizontal pump suction for all 4 pumps. The engineer thought concentric looked “cleaner” and saved material cost. But on a horizontal liquid suction line, the concentric reducer creates a flat-top shoulder that traps a continuous air pocket at the high point. This air pocket: (1) caused vortexing and air ingestion into the pump, (2) reduced net positive suction head available (NPSHa), (3) led to cavitation and impeller damage.
Step 3 — Correct retrofit
Replace all 4 concentric reducers with eccentric reducers flat-side-up (top of pipe stays flat, bottom tapers up):
• Eccentric reducer DN300 × DN250, 316L, Schedule 40, ASME B16.9, BW end
• Orientation: flat side on TOP (top of pipe stays horizontal — no air pocket)
• The eccentric reducer eliminates the high point — air flows freely to the pump and gets swept through
• Same material (316L) and wall thickness (S40) as the existing line — no welding qualification needed
• Replaced the worn impeller on pump #2 during the same outage
Step 4 — Outcome
• The retrofit was a small parts-only intervention — four off-the-shelf 316L eccentric reducers plus four field welds, all done within one planned outage
• Pump flow on units #1, #2, #3 recovered to nameplate within two weeks of recommissioning
• No further impeller pitting observed on the remaining units after 18 months of follow-up
• The retrofit cost a small fraction of a single-day plant shutdown, and avoided what would have been a cascading impeller failure across all four pumps
• Lesson: on horizontal pump suction liquid lines, ALWAYS use an eccentric reducer installed flat-side-up — concentric is only for vertical lines and gas lines
Why EPC Contractors Specify Pipe Fittings with Chuanglan
DN15–DN600 elbows (90° / 45°), equal / reducing tees, concentric / eccentric reducers, caps, stub ends
304 / 304L / 316 / 316L / A234 WPB · Schedule 10S / 40S / 80S / 160 · BW / SW / threaded / tri-clamp ends
ASME B16.9 · B16.11 · EN 10253 · JIS B2312 · DIN 2605/2615/2616 · EN 10204 3.1 MTC · ISO 15156 on request
Need Help Specifying Pipe Fittings?
Tell us your fitting type, size, Schedule, material (304 / 316L), end connection, and standard — our engineers will review your piping isometrics and recommend the right fittings (including concentric vs eccentric reducers) within 24 hours.
Get Free Sizing Report → WhatsApp us5. Key Standards You Need to Know
| Standard | Region | What It Covers |
|---|---|---|
| ASME B16.9 | USA / International | Butt-weld fittings (elbows, tees, reducers) — dimensions, tolerances |
| ASME B16.11 | USA / International | Socket-weld and threaded fittings (small sizes, high pressure) |
| EN 10253 | Europe | European butt-weld fittings dimensions and technical delivery conditions |
| JIS B2312 | Japan | Japanese butt-weld fittings dimensions |
| DIN 2605 / 2615 / 2616 | Germany / Europe | German standard fittings (elbows, tees, reducers) |
Most common: ASME B16.9 for butt-weld fittings (global standard). Always specify the standard when ordering — dimensions differ between standards (e.g., a 2″ elbow to ASME B16.9 has a different center-to-end length than a DIN elbow).
6. Schedule (Wall Thickness) Selection
Pipe fittings come in different wall thicknesses, called “Schedule.” The higher the schedule number, the thicker the wall, and the higher pressure it can handle.
| Schedule | Wall Thickness (for 2″ pipe) | Pressure Rating | Best For |
|---|---|---|---|
| Schedule 10S | 1.65 mm | Low (PN10 max) | Sanitary, thin wall, low pressure, food / pharma |
| Schedule 40S / 40 | 3.91 mm | Medium (PN40 / Class 300) | Most common, general industry, water, oil |
| Schedule 80S / 80 | 5.54 mm | High (PN100 / Class 600) | High pressure, oil & gas, steam |
| Schedule 160 | 8.74 mm | high (Class 900+) | Extreme pressure, special applications |
Most common: Schedule 40 for general industrial use (about 70% of applications). Schedule 10S for sanitary / food. Schedule 80 for high pressure / oil & gas. Match the fitting Schedule to the pipe Schedule — they must be the same for proper butt-weld joint fit-up.
7. Concentric vs Eccentric Reducers: Which One?
| Application | Reducer Type | Why |
|---|---|---|
| Pump suction (horizontal) | Eccentric reducer (flat side up) | Prevents air pockets from forming at the pump |
| Oil pipeline (horizontal) | Eccentric reducer (flat side up) | Prevents vapor accumulation |
| Vertical piping | Concentric reducer | No air pocket risk in vertical lines |
| Gas pipeline | Concentric reducer | Gas doesn’t pool, no need for eccentric |
This is one of the most common mistakes people make — choosing the wrong type of reducer.
Concentric reducer: Both ends are centered on the same axis (like a cone). Use this for vertical piping, gas lines, or any line where liquid doesn’t accumulate.
Eccentric reducer: One side is flat (the centerlines are offset). Use this for horizontal liquid lines (pump suction, oil lines, water lines). The flat side goes on top — this prevents air pockets from forming, which can damage pumps or cause flow problems.
8. Buying Checklist
When you send an RFQ for stainless steel pipe fittings, include:
- Fitting type (elbow 90° / elbow 45° / tee / reducer / cap / stub end)
- Size (nominal bore / OD, inches or DN)
- Schedule / wall thickness (S10 / S40 / S80 / S160)
- Material (304 / 304L / 316 / 316L / A234 WPB)
- End connection (butt-weld / socket-weld / threaded / tri-clamp)
- Standard (ASME B16.9 / B16.11 / EN 10253 / JIS / DIN)
- Quantity of each size and type
- Required certifications (MTC / EN 10204 3.1)
9. Southeast Asia & Middle East Market Notes
For clients in Southeast Asia (Thailand, Vietnam, Indonesia, Malaysia, Singapore, Philippines), water treatment, food & beverage, brewery, palm-oil, and chemical plants predominantly specify ASME B16.9 butt-weld fittings in 304 / 304L Schedule 40 for general service. Vietnamese and Thai water treatment plants (Thu Duc, MWA, PWA) require full EN 10204 3.1 MTC on every fitting. Indonesian palm-oil refineries and Malaysian petrochemical plants often specify carbon steel A234 WPB S40 / S80 fittings for oil and steam service, with 304 / 316L for product lines. Singaporean and Malaysian offshore projects require 316L with ISO 15156 sour-service certification. Food, brewery, and dairy plants (Thai Union, Vinamilk, Indonesian breweries) specify sanitary tri-clamp sanitary pipe fittings in 316L with interior RA ≤ 0.8 μm finish.
For clients in the Middle East (Saudi Arabia, UAE, Qatar, Kuwait, Oman, Bahrain), oil & gas, petrochemical, SWRO desalination, power, and district-cooling projects (Saudi Aramco, ADNOC, SABIC, SEC, DEWA, QP, KOC) universally require ASME B16.9 / B16.11 fittings with full EN 10204 3.1 MTC and often ISO 15156 sour-service certification. Carbon steel A234 WPB / WPHY fittings are standard for oil, gas, and steam; 316L (NOT 304) is mandatory for any wetted fitting in seawater, brine, or coastal service — Jubail, Yanbu, Dammam, Abu Dhabi, Dubai, and Ras Al Khaimah plants all require 316L due to high Gulf chloride content. For SWRO brine discharge lines, pair 316L butt-weld fittings with 316L lap-joint flanges and 316L stub ends.
Chuanglan Valve supplies butt weld pipe fittings (90° / 45° elbows, equal / reducing tees, concentric / eccentric reducers, caps, stub ends) in 304 / 304L / 316 / 316L / A234 WPB, Schedule 10S / 40S / 80S / 160, ASME B16.9 / B16.11 / EN 10253 / JIS B2312 standards, with full MTC EN 10204 3.1 certificates. Serving EPC Contractors Across Southeast Asia & Middle East · ISO 9001:2015 · Established in 2009 · MOQ 1 piece.
Common Fitting Selection Mistakes
Mixing Schedule 40 and Schedule 80
Socket weld and butt weld fittings must match the pipe schedule. Mismatched schedules cause leak paths.
Using 304 in coastal/desalination service
304 resists atmospheric corrosion but fails in chloride environments. Use 316L for any seawater or brackish water application.
Ignoring end prep requirements
Butt weld fittings need beveled ends and proper gap. Socket weld fittings require 1/16-inch expansion gap. Read the drawing before welding.
FAQ
What is the difference between butt-weld and socket-weld fittings?
Butt-weld (BW) fittings have the same OD as the pipe and are welded directly onto the pipe end with a full-penetration weld — used for DN50 and up, high pressure / temperature, and permanent joints. Socket-weld (SW) fittings have a socket recess that the pipe slides into, then a fillet weld is made around the outside — used for small sizes (DN50 and under) and high pressure (Class 300–2500). BW is cheaper for large sizes; SW is easier to align for small high-pressure lines.
Can I mix ASME B16.9 fittings with EN 10253 pipe?
Butt-weld fittings are welded to pipe, so the connection is made by welding — the fitting OD must match the pipe OD. ASME B16.9 fittings are sized for ASME pipe (NPS schedule), while EN 10253 fittings are sized for EN / DIN pipe (DN). If you mix standards, the OD and wall thickness won’t match, causing poor weld fit-up. Always specify the standard of BOTH pipe and fittings.
Why is Schedule 40S different from Schedule 40?
Schedule 40 (without “S”) is for carbon steel pipe per ASME B36.10M. Schedule 40S (with “S”) is for stainless steel pipe per ASME B36.19M. They have the same OD but slightly different wall thicknesses for some sizes. Always use the “S” version for stainless fittings and pipe — mixing S and non-S causes wall mismatch at the weld.
What is a stub end and why do I need it?
A stub end is a short butt-weld piece (with a raised lap) that welds to the pipe and slips inside a loose lap-joint flange. The loose flange rotates freely and is never wetted. Use stub ends when: (1) the pipe is expensive 316L and you want to save money (loose flange body can be 304L or carbon steel), or (2) you need frequent disassembly for alignment. Always match the stub end to the flange standard (ASME B16.5 or EN 1092-1).
How do I specify an eccentric reducer orientation?
Always specify “flat side up” (FSO) for horizontal liquid service. In writing, note: “eccentric reducer, flat side up (top of pipe horizontal).” This is critical for pump suction lines — if you install it flat-side-down, you create a low point that traps sediment and causes the same air-pocket problem. Welders often install eccentric reducers in the wrong orientation if not clearly specified.
Do you supply fittings with interior polishing for sanitary use?
Yes. We supply sanitary 316L fittings (elbows, tees, reducers, unions) with interior electropolished finish RA ≤ 0.8 μm (or 0.5 μm for pharma), tri-clamp ends, and full 3.1 certificates including surface-finish test reports. These are used for brewery, dairy, pharma, and biotech CIP / SIP systems.
What is the lead time from Chuanglan?
Standard butt-weld fittings (DN15–DN300, S40S, 304 / 316L, BW) are in stock and ship in 7–15 days. Large sizes (DN350–DN600+), high pressure (S80S / S160), special alloys, sanitary finishes, and special standards take 15–30 days. We export to Indonesia, Malaysia, Thailand, Vietnam, Singapore, Saudi Arabia, UAE, and more.
References & Standards
- ASME B16.9: Factory-Made Wrought Buttwelding Fittings
- ASME B16.11: Forged Fittings — Socket Welding and Threaded
- EN 10253: Butt-welding fittings (Europe) — dimensions and tolerances
- JIS B2312: Stainless steel butt-welded fittings (Japan)
- DIN 2605 / 2615 / 2616: German standard elbows, tees, and reducers
Related Products
Continue Reading
Request a Quotation — Reply Within 24 Hours
Send your line size, pressure rating, medium and quantity. Our engineers come back with price, drawing and lead time — no obligation.